
Engine valves
TripleHard® on engine valve stems
For engine valve stems, TripleHard® has been tested and is offered for licensed production on an existing line converted from Cr(VI).
Hard-chrome-level hardness as plated, hardness maintained after heat cycling to 500 °C, and no measurable attack in hot acid after heat treatment. Made in a Cr(III) hard-chrome process.
- 0 µm
- attack in 5 % H₂SO₄ at 100 °C, 23 min, after heat treatment
- 5–10 µm
- coating thickness on the stem
- 500 °C
- heat cycling: hardness is maintained
Why engine valves
A valve stem lives in heat, acid and motion.
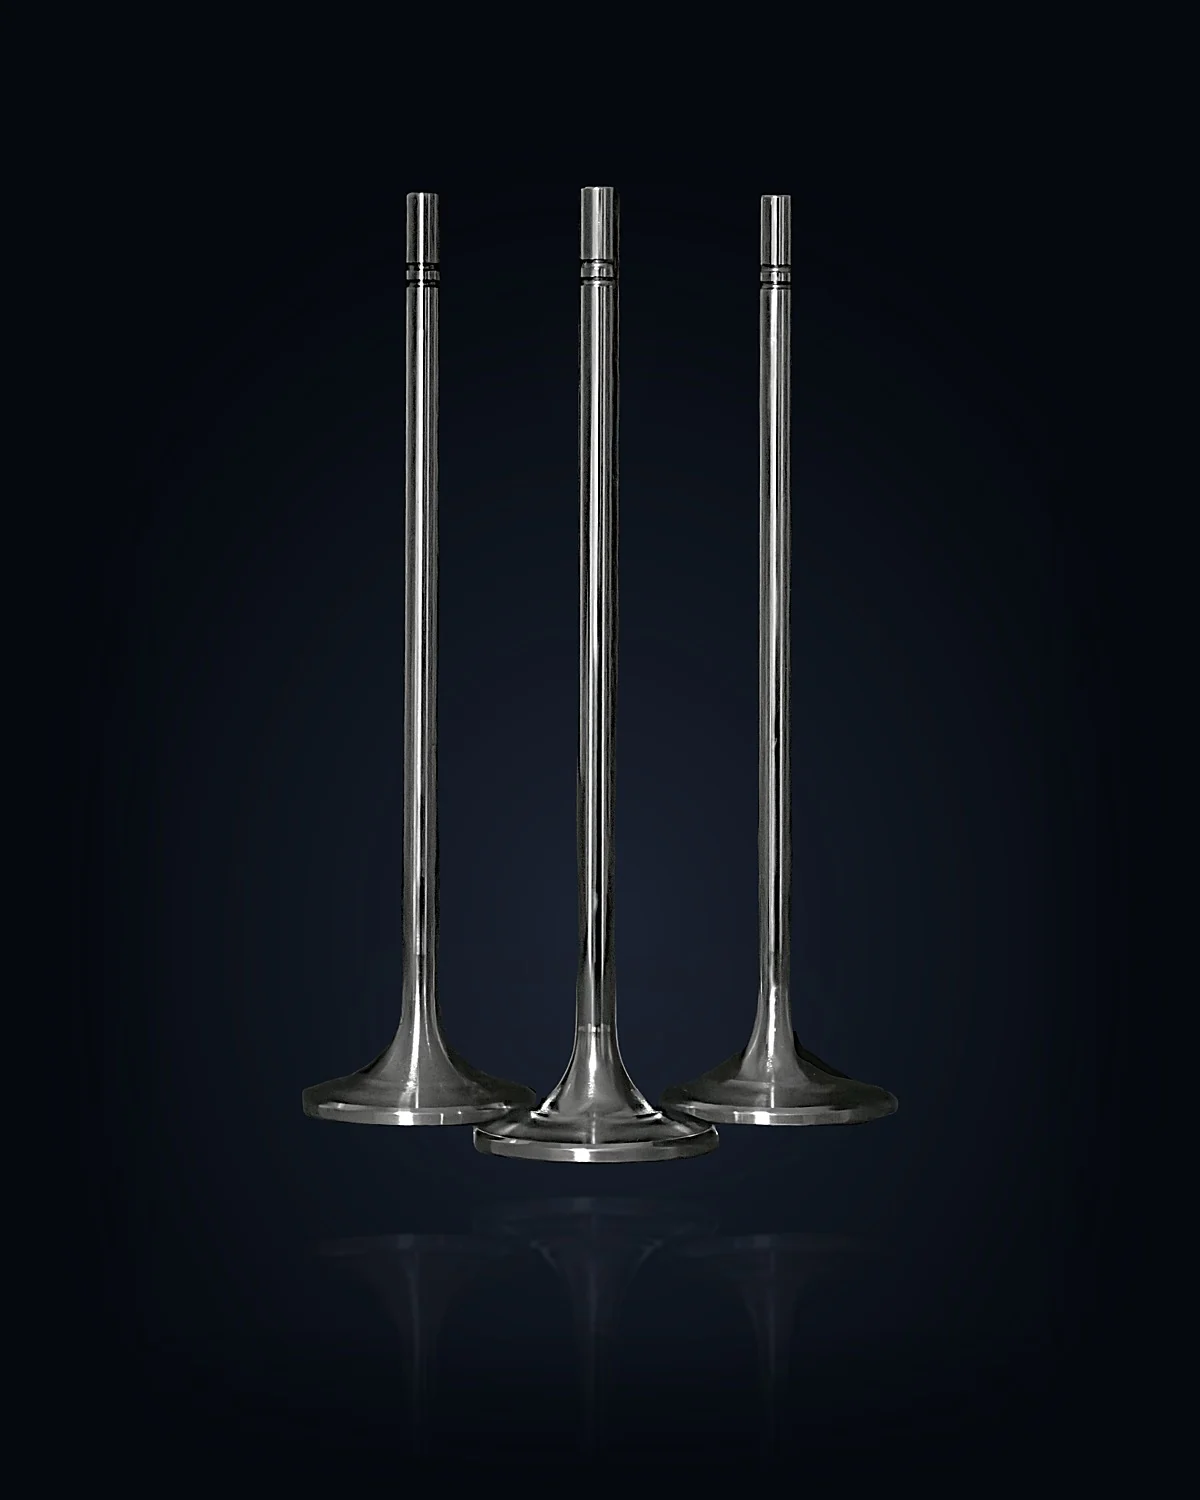
The stem slides in its guide millions of times, at exhaust temperature, in combustion by-products that are acidic. The coating has to stay hard, stay attached and stay thin.
- Heat. Hardness rises, rather than falls, after heat cycling to 500 °C; in Cr(VI) hard chrome it falls as the temperature rises.
- Acid. 0 µm attack in 23 min of 5 % H₂SO₄ at 100 °C after heat treatment, which simulates valve service; the Cr(VI) references, not heat-treated, lost 7–22 µm in 2–22 min
- Adhesion. Intact after bend and scratch testing
- Thickness. 5–10 µm on the stem, set from your drawings
How it is produced
On a converted line.
Current Tested on valve stems; offered for licensed production on a converted line, in open tanks or a coating cell of their own, not on the continuous line. Volume production is possible there but has not started. Results here are coating tests on specimens and parts.
Engine valves are plated on your existing line, converted: a TripleHard® Cr(III) bath replaces the Cr(VI) bath and a nickel bath is added where the line has none. Savroc supplies the process and the support, and simulates and engineers each conversion for your parts.
Read the technology page How a project works- Changes in a conversion
- Carries over from the existing line
- Carries overHoist and railThe existing hoist carries the part from tank to tank.
- Carries over1 · Surface preparationCleaning, as on the existing line.
- Carries over2 · EtchingActivates the steel surface, as on the existing line.
- Changes3 · Nickel anchor layerA nickel bath is added where the line has none.
- Changes4 · TripleHard® Cr(III) bathReplaces the Cr(VI) bath with a TripleHard® Cr(III) bath.
- Carries overRinses and handlingThe rinse after each stage and the existing handling stay as they are.
Technical package
What is measured.
Full test conditions and the regulatory position are on the technology page.
| Acid resistance | 5 % H₂SO₄, 100 °C, 23 min: 0 µm, 0 g mass loss, after heat treatment simulating valve service at around 500 °C (Cr(VI) references not heat-treated) |
|---|---|
| Thermal behaviour | Hardness is maintained after heat cycling to 500 °C |
| Adhesion | Bend and scratch test without delamination |
| Hardness | Hard-chrome level, full hardness without heat treatment |
| Coating thickness | 5–10 µm on the stem |
Frequently asked questions
What does a plater need to change?
The chemistry and its control: the Cr(VI) bath becomes a TripleHard® Cr(III) bath and a nickel bath is added where the line has none. Tanks and handling largely carry over; the full conversion specification is part of the plan Savroc engineers for your line.
How thick is the coating on a valve stem?
Typically 5–10 µm. The exact thickness is set from your drawings for the stem, its guide and its duty, and verified during commissioning.
Contact
Ready to start your move off hexavalent chromium?
Talk to us about your parts and the targets they must meet. A first conversation needs no drawings.